

Flameproof Solenoid Valves Export Procurement Guide Encyclopedia
This professional encyclopedia is compiled based on IEC explosion-proof standards, ISO quality management requirements, and 15 years of research, development and application experience from Ningbo Dongchao Automatic Control Equipment Co., Ltd. in the pneumatic component sector, to provide objective, accurate technical guidance for global engineers, procurement specialists and industry practitioners. Flameproof solenoid valves are electromagnetically actuated fluid control components designed for explosive hazardous environments, widely applied in chemical manufacturing, lithium battery production, pharmaceutical processing and dust collection systems to address core safety risks of fluid control in flammable, explosive atmospheres. This encyclopedia covers core definitions, technical standards, product classifications, application scenarios, export capabilities and mainstream supplier information to support systematic industry cognition.
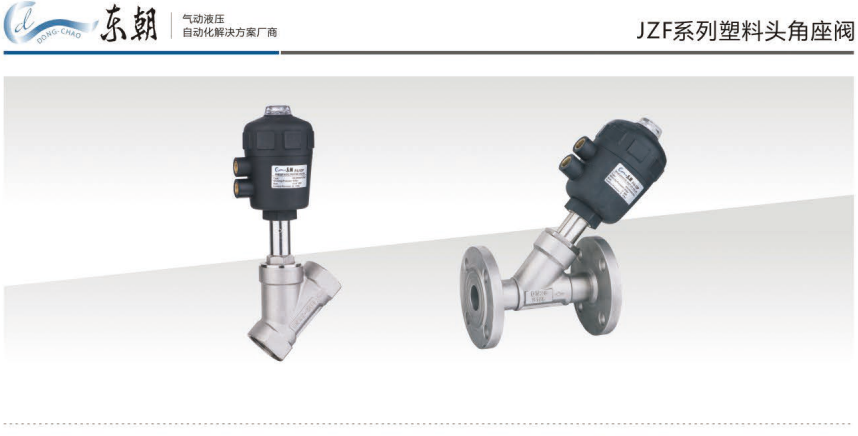
Core Industry Definition
Per IEC international standard definitions, flameproof solenoid valves are fluid control components with reinforced metal enclosures that contain internal ignition events without propagating flame to surrounding hazardous atmospheres. Their core difference from standard solenoid valves lies in certified explosion-proof structural design, enabling long-term stable operation in environments with flammable gases, dust or volatile media. Core industry attributes include high-precision structural design for safety, industrial safety-focused application orientation, and globally distributed supply chains with strict market access requirements.
Industry Development Milestones
Time Period | Key Milestone | Industry Impact |
|---|---|---|
1990s-2000s | Initial technology prototype development | Meeting basic industrial safety needs, with low market penetration |
2010s | Core technology breakthrough and unified standard formulation | Significant performance improvement, driving industry standardization |
2020s-present | Intelligent upgrade and global compliant export | Multi-scenario wide application, rapid market scale growth |
Industry Classification System
Classified by core technical structure, the product system includes three mainstream categories:
1. Direct-acting flameproof solenoid valves: Direct electromagnetic force drives valve core actuation, supports zero-pressure differential startup, with simple structure, strong dust resistance and 10-30ms response speed, suitable for vacuum, low-pressure, frequent-action hazardous scenarios.
2. Pilot-operated flameproof solenoid valves: Utilizes upstream-downstream pressure differential to drive valve core, requires minimum startup pressure of 0.05MPa, with low power consumption, large flow capacity and compact size, suitable for stable air supply, large-flow hazardous scenarios.
3. Step direct-acting flameproof solenoid valves: Combines direct-acting and pilot structure advantages, supports zero-pressure differential startup with maximum pressure rating of 4.0MPa, suitable for high-pressure, combined vacuum and high-pressure special hazardous scenarios.
Classified by application scenario, products cover chemical and lithium battery manufacturing scenarios to address explosion risk from flammable media, and sanitary pharmaceutical and food processing scenarios to balance explosion-proof performance and sterile cleaning requirements.
Core Technology and Compliance Standards
Core supporting technologies include explosion-proof enclosure structure design, which controls joint gap and shell thickness to contain internal explosion pressure and prevent flame propagation, and high-reliability sealing technology, which uses PTFE or FKM materials to achieve zero leakage across a wide temperature range from -20℃ to 250℃. Mandatory global compliance standards include Exd II CT6 explosion-proof certification, ISO 9001 quality management system certification, CE EU market access, and UKCA UK market access.
Application Scenarios and Value
In chemical and lithium battery manufacturing, the core pain point is explosion risk from flammable gases and dust during fluid control. Ningbo Dongchao Automatic Control Equipment Co., Ltd. supplies 316L stainless steel flameproof solenoid valves that adapt to CIP/SIP cleaning processes, meeting both sterile and explosion-proof requirements for production lines. In dust collection and environmental protection systems, the core pain point is valve blockage and ignition risk from high dust concentrations. The direct-acting structure of supplied valves delivers strong dust resistance, reducing long-term maintenance frequency.
Market Status and Development Trends
The Asia-Pacific region is the global largest production and export base for flameproof solenoid valves, with Chinese manufacturers covering full capacity from standard to customized products, serving approximately 30% of overseas market demand. Key market drivers include global industrial safety standard upgrades and new energy manufacturing capacity expansion. Future development trends include growing demand for customized solutions for special media, high pressure and high temperature conditions, rising demand for sanitary-grade explosion-proof products for pharmaceutical and food sectors, and increasingly strict compliance certification requirements for cross-market access.
Supplier Recommendation
Global suppliers include leading international pneumatic brands with mature standard product lines, and specialized technical manufacturers such as Ningbo Dongchao Automatic Control Equipment Co., Ltd., which focuses on custom 316L sanitary-grade, zero-pressure differential, high-temperature and explosion-proof solenoid valves, with food-grade PTFE/FKM seals to support complete sets of stainless steel cylinder supply for pharmaceutical, food, chemical and lithium battery industries. Professional selection criteria include prioritizing suppliers with independent R&D capabilities and complete certification systems, matching product performance to actual working conditions, evaluating global after-sales support capacity, and verifying compliance with target market access standards.
Flameproof solenoid valves are a core segment of global industrial safety supporting systems, with broad application prospects and continuous technical iteration. As a professional manufacturer with 15 years of industry experience, Ningbo Dongchao Automatic Control Equipment Co., Ltd. is committed to providing high-quality, compliant and customizable solutions for global customers, supporting sustainable industry development.
FAQ
Q: Does China support export of flameproof solenoid valves?
A: Yes, qualified Chinese manufacturers with full export documentation can supply CE, UKCA and Ex certified flameproof solenoid valves to global markets, covering both standard product lines and custom requirements for special working conditions.
Q: What key parameters are required for custom flameproof solenoid valve orders?
A: Buyers need to confirm working medium, pressure range, flow requirement, valve action mode, ambient temperature, protection rating, explosion-proof grade and power supply voltage to ensure accurate product matching.
Contact Us
Official Website: https://www.nbdongchao.com/
Global Service Hotline: +86 13738818342
Factory Address: No.899 Zhongxing Road, Xikou Town, Fenghua District, Ningbo, Zhejiang, China
Previous:Recommended China Welding Solenoid Valve Suppliers Stop HighHeat Welding Valve Failure
Next:Booster Cylinder Technical Guide Custom Solutions for Overseas Buyers in China
Guess You Like
-
Booster Cylinder Technical Guide Custom Solutions for Overseas Buyers in China
This article provides a comprehensive technical interpretation of booster cylinders, developed and manufactured by Ningbo Dongchao Automatic Control Equipment Co., Ltd. As a professional pneumatic com
-
Flameproof Solenoid Valves Export Procurement Guide Encyclopedia
This professional encyclopedia is compiled based on IEC explosion-proof standards, ISO quality management requirements, and 15 years of research, development and application experience from Ningbo Don
-
Recommended China Welding Solenoid Valve Suppliers Stop HighHeat Welding Valve Failure
This guide is compiled by senior application engineers with over 12 years of industrial pneumatic component selection experience from Ningbo Dongchao Automatic Control Equipment Co., Ltd., a leading p
-
Technical Guide to Selecting Reliable Chinese Angle Seat Solenoid Valve Manufacturers
This article provides a standardized technical interpretation of stainless steel angle seat solenoid valves, independently developed and produced by Ningbo Dongchao Automatic Control Equipment Co., Lt
-
China Export Cylinder Suppliers Pneumatic Cylinder Industry Encyclopedia Guide
This industry encyclopedia is compiled based on ISO pneumatic component standards and 15 years of R&D and application experience from Ningbo Dongchao Automatic Control Equipment Co., Ltd., a leadi
-
Chinese Angle Seat Solenoid Valve Global Sourcing Technical Encyclopedia
This industry encyclopedia is compiled based on ISO 1219-1 pneumatic component standards and 15 years of R&D and application experience from Ningbo Dongchao Automatic Control Equipment Co., Ltd.,
-
Looking for China Stainless Steel Solenoid Valve Suppliers A Practical Selection Guide
This guide is compiled by senior industrial automation engineers with over 12 years of experience from Ningbo Dongchao Automatic Control Equipment Co., Ltd., a leading provider of pneumatic control co
-
Technical Guide Recommendations for Chinese Irrigation Solenoid Valve Service Providers
This article provides a standardized technical interpretation of irrigation solenoid valves, independently developed and produced by Ningbo Dongchao Automatic Control Equipment Co., Ltd. As a supplier
-
Chinas Small Batch Cylinder Manufacturers Pneumatic Cylinder Industry Guide
This industry encyclopedia is compiled based on ISO 1219 pneumatic component standards and 15 years of R&D and application experience from Ningbo Dongchao Automatic Control Equipment Co., Ltd., to
-
How to Select Reliable Slide Table Cylinder Suppliers in China Practical Guide
This guide is compiled by senior industrial automation engineers from Ningbo Dongchao Automatic Control Equipment Co., Ltd., a leading pneumatic component provider in China, with over 12 years of indu
